Featured OEM Quartz Glass Components & Manifold Blocks
Direct factory fabrication from Donghai County, China's crystal capital. Every product is produced according to technical 2D/3D schematics with flame-working, CNC laser trepanning, and optical annealing.
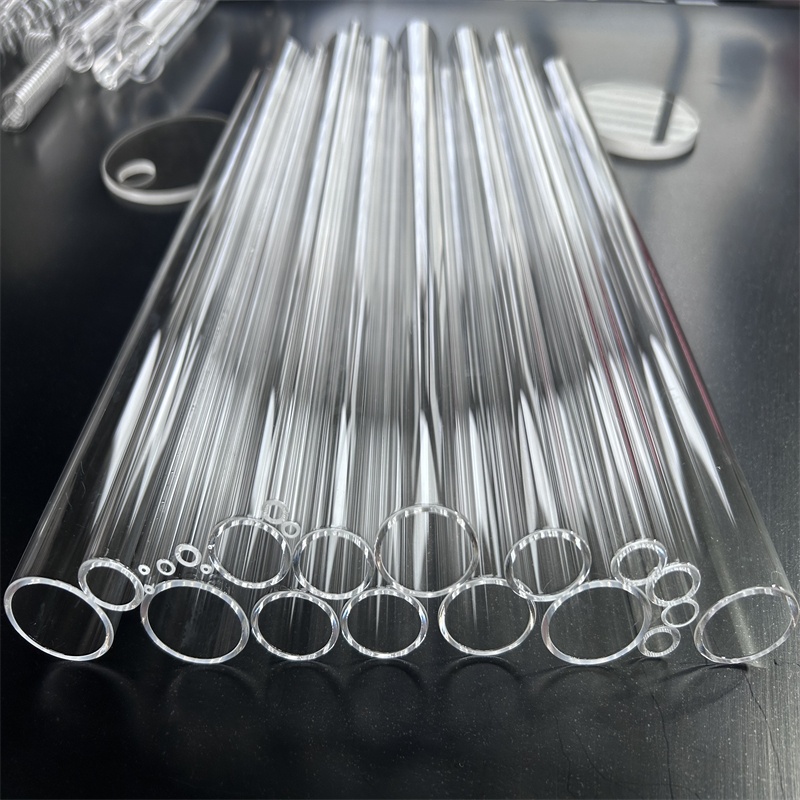
High Temperature Clear 99.99% Pure Fused Quartz Twin Tube
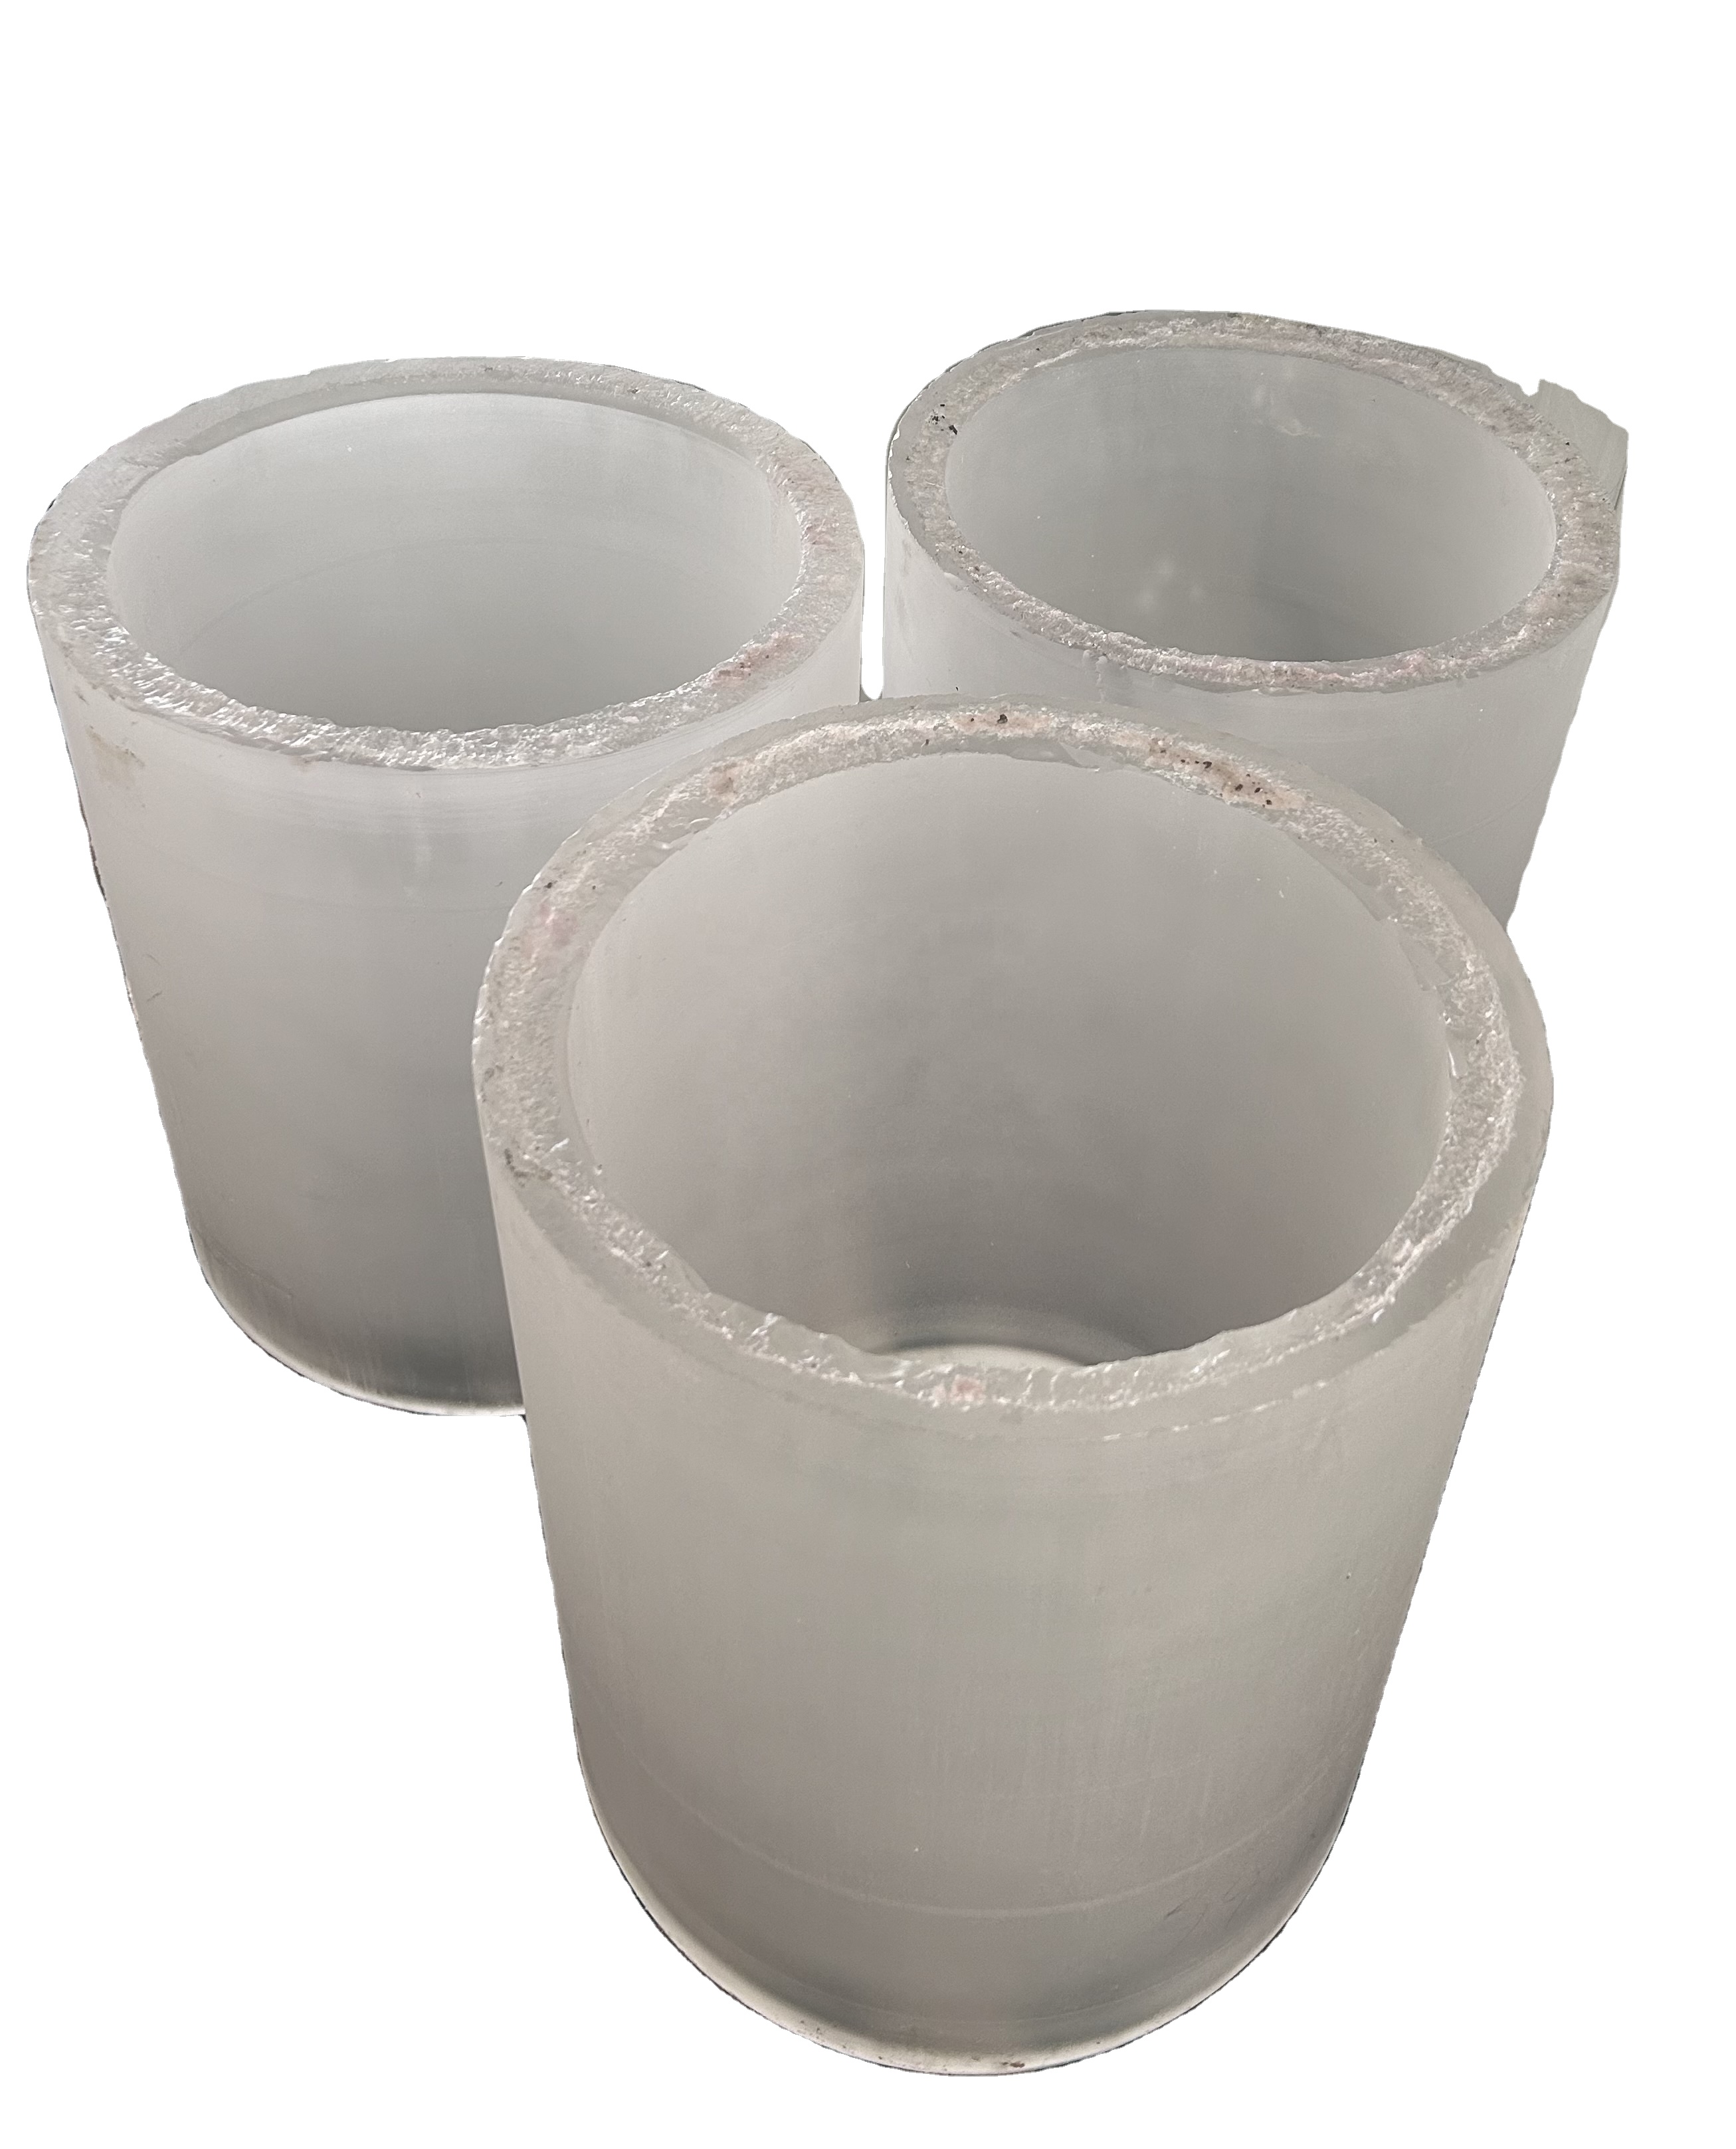
Open Ended Fused Quartz Frosted Cylinder & Ingot
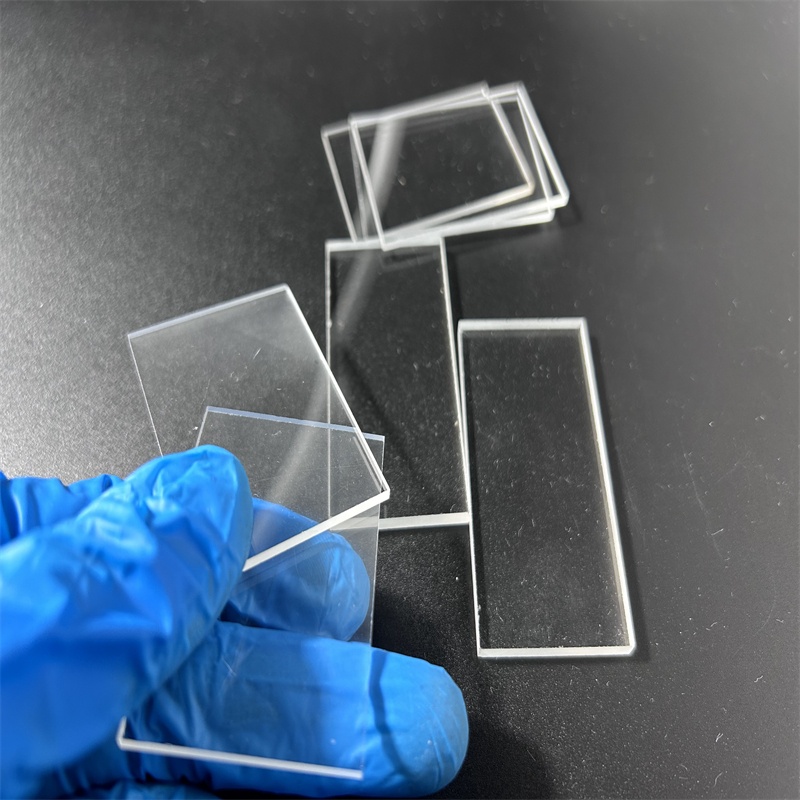
Transparent Fused Quartz Glass Sheet & Windows
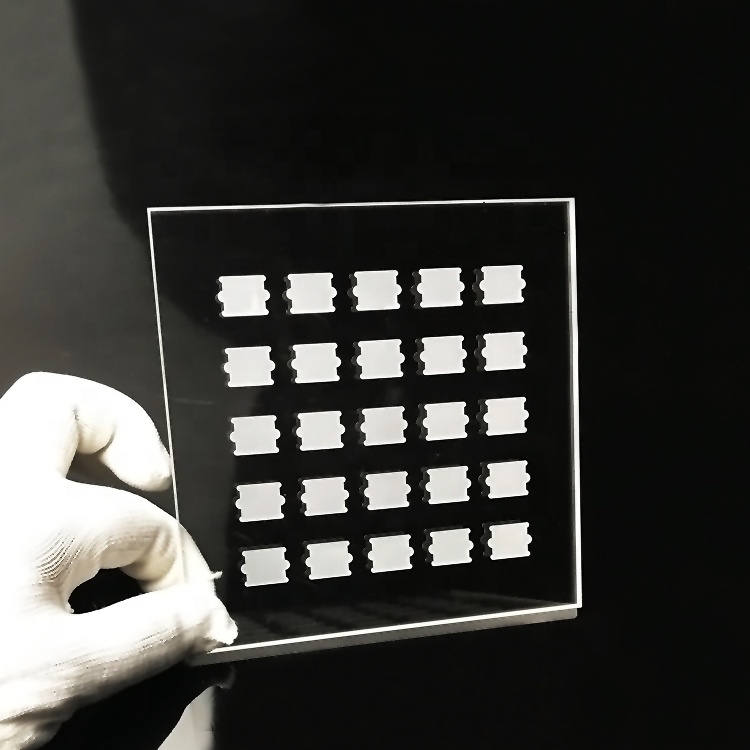
Circular Fused Quartz XRD Sample Holder Plate
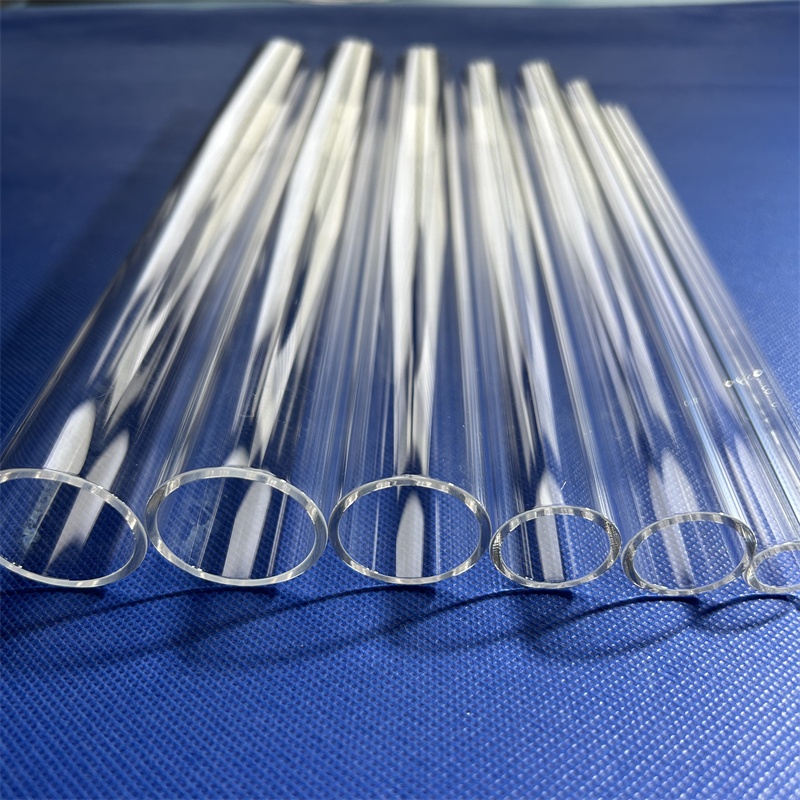
High Pressure Pure Quartz Tube for Furnace & Boiler
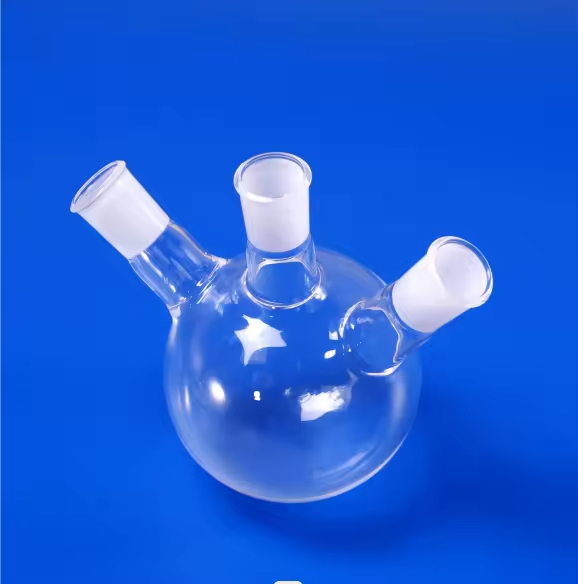
Twin-Tube Bottom Flask with Custom Weld Ports
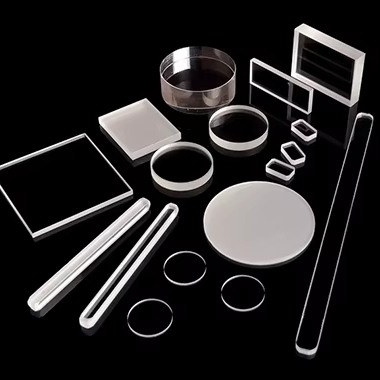
Optical Grade Test Sample Quartz Sheet & Substrate
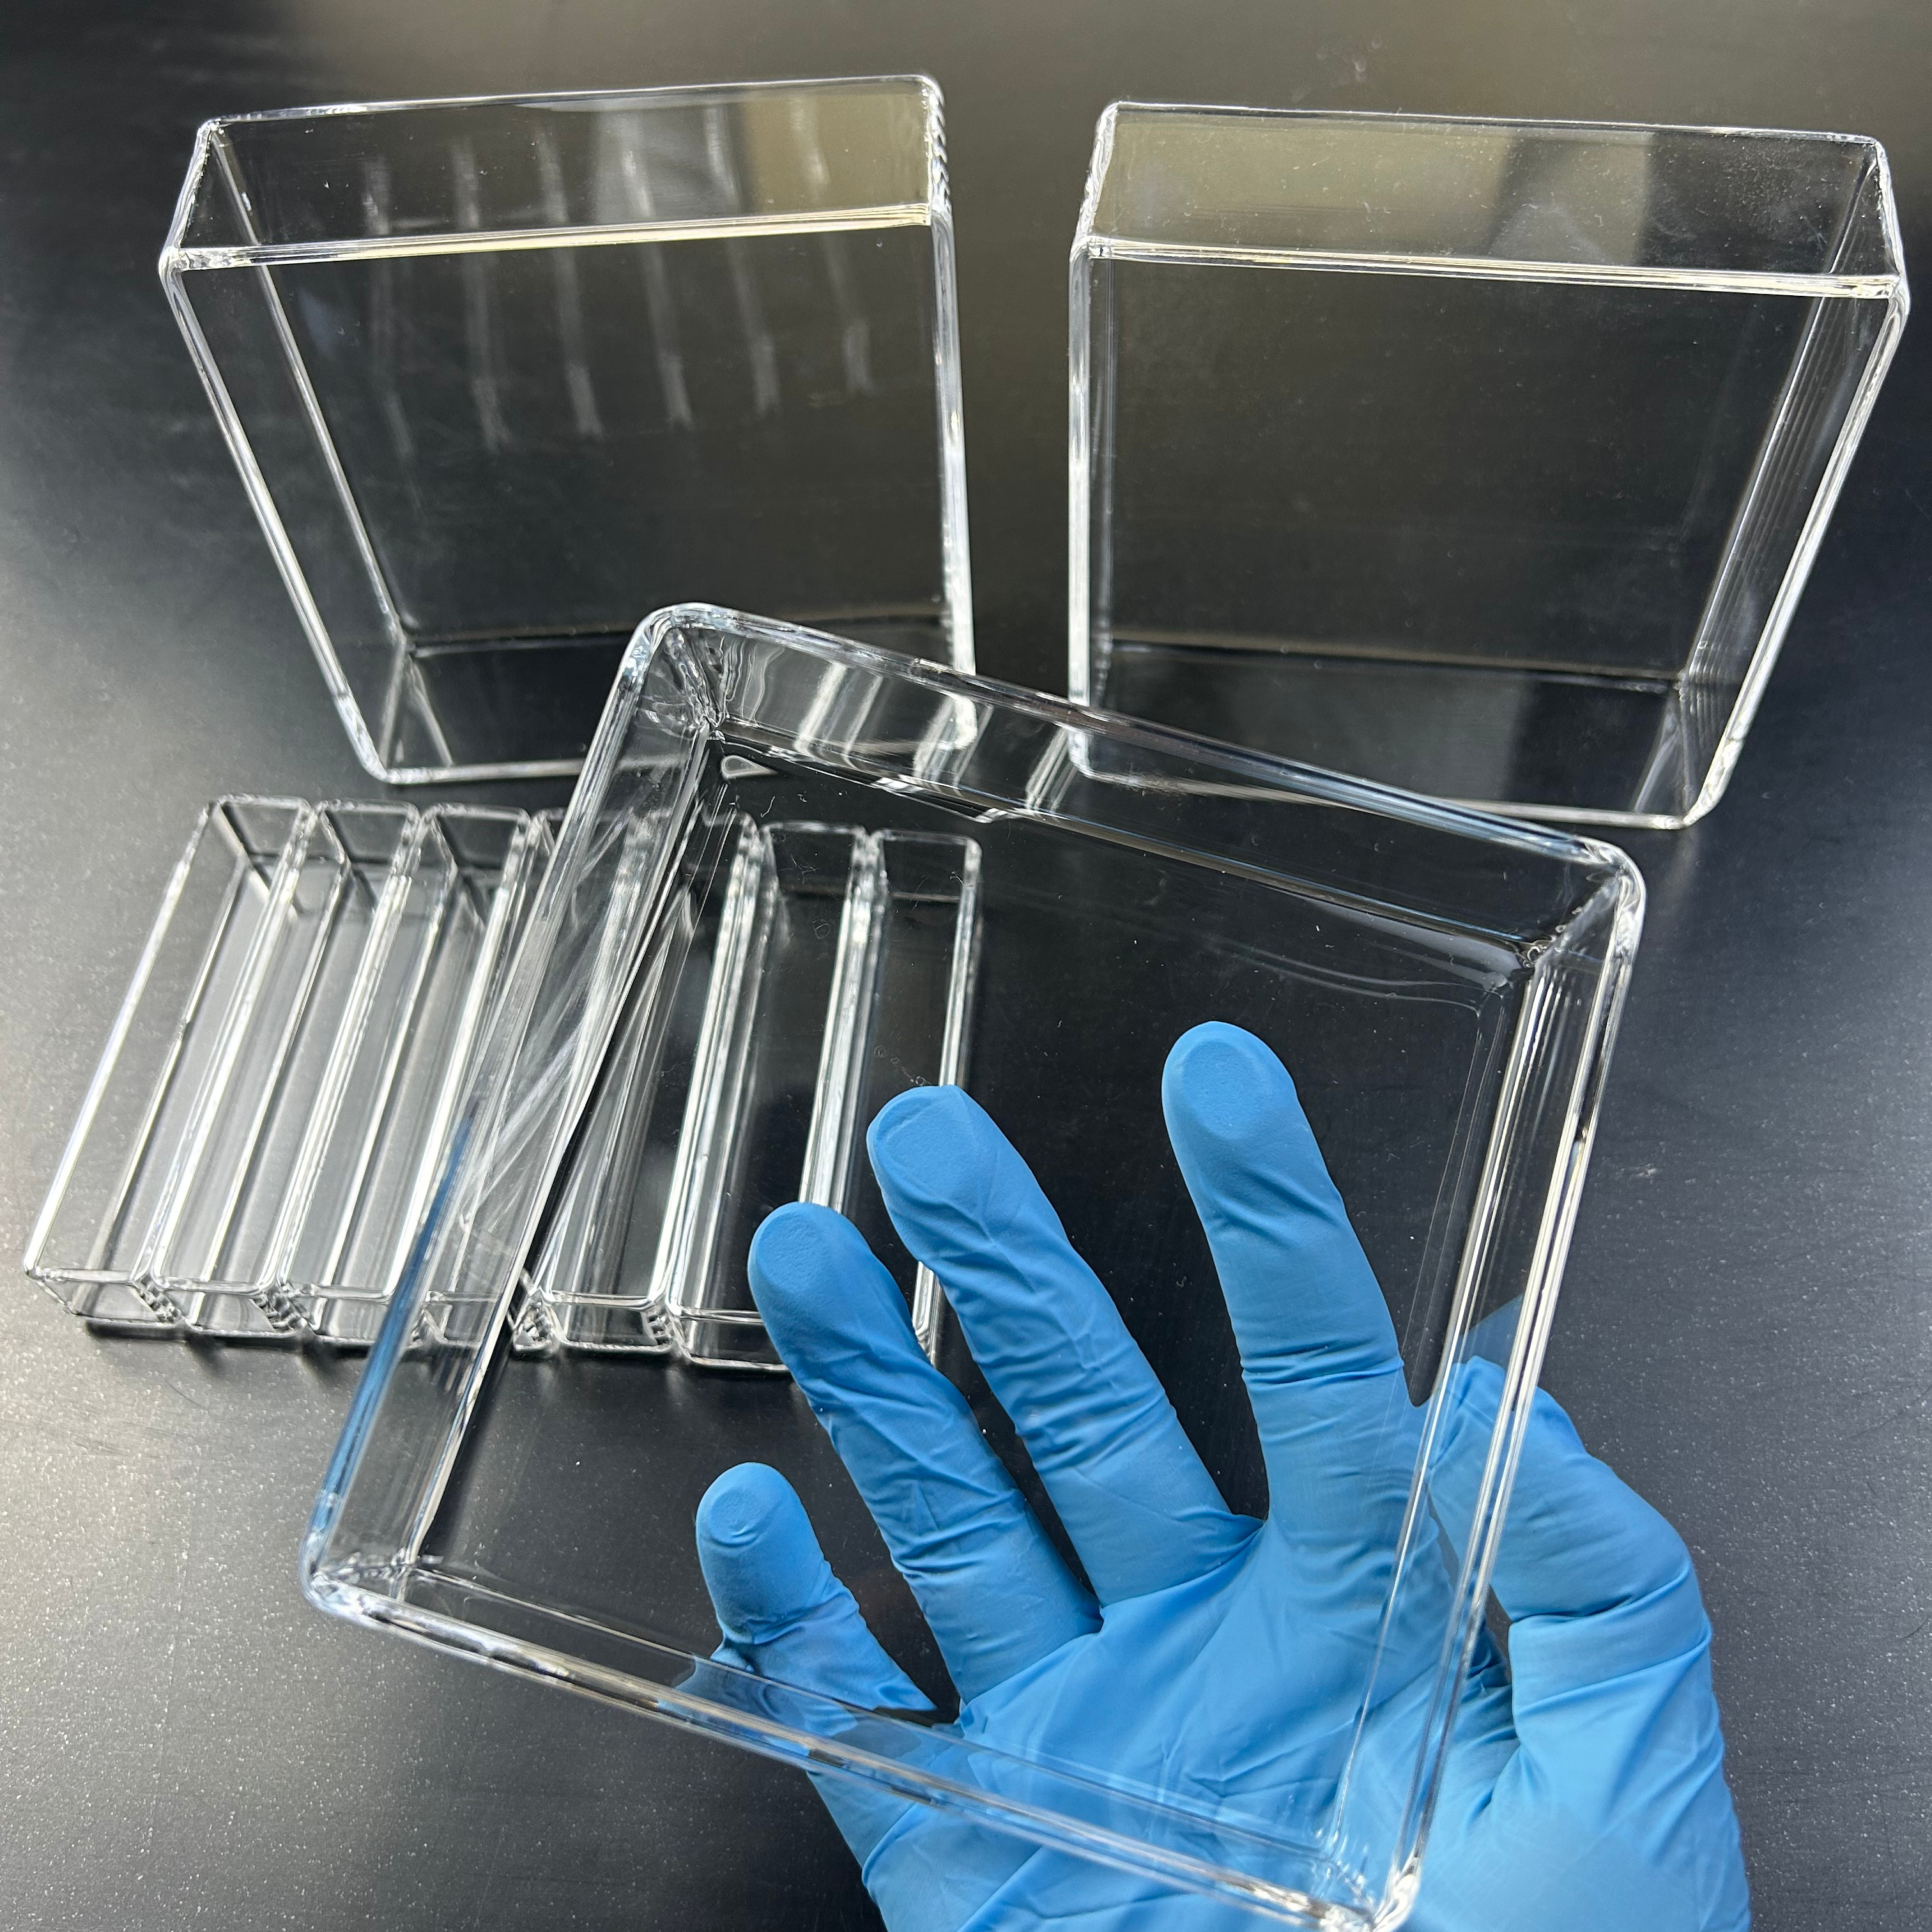
Fused Quartz Circular Cylinder Crucible & Reaction Tank
Engineering High-Purity Quartz Glass Manifolds: Fluidics, Metallurgy, & Plasma Resistance
An in-depth analysis of custom OEM fused quartz distribution assemblies for Atomic Layer Deposition (ALD), Chemical Vapor Deposition (CVD), and corrosive chemical dosing systems.
1. The Critical Role of Fused Silica Manifolds in Semiconductor & Chemical Routing
In modern thin-film semiconductor processing, reactive ion etching (RIE), and high-purity biopharmaceutical chromatography, fluid handling infrastructure is subjected to intense operational stresses: aggressive halide gases (fluorine, chlorine, bromine compounds), ultra-high thermal cycling exceeding 1,100°C, and the uncompromising mandate for sub-ppb (parts-per-billion) trace metal purity. Traditional high-nickel alloys and fluoropolymer manifolds (such as PTFE or PFA) experience severe thermal deformation, fluorination leaching, or micro-particulate shed under high-energy plasma regimes.
Custom OEM quartz glass manifolds solve these systemic vulnerability points. Fabricated from natural fused quartz or synthetic fused silica with silicon dioxide (SiO2) concentrations of 99.99% to >99.999%, these multi-channel monolithic and welded headers provide total chemical inertness against virtually all acids (except hydrofluoric and hot concentrated phosphoric acid). Their near-zero coefficient of thermal expansion (α = 5.5 × 10⁻⁷ /K) delivers unmatched thermal shock resistance, allowing manifold assemblies to tolerate instantaneous temperature gradients of over 1000°C without volumetric cracking, mechanical shear, or micro-fracture propagation.
A quartz glass manifold assembly typically consists of a primary distribution plenum seamlessly integrated with multiple precision intake and output ports, bypass metering lines, and vacuum flange couplings (KF/NW, CF, or spherical ball joints). Fabricating these intricate assemblies requires mastering three interdependent disciplines: CNC diamond micro-machining, laser-guided trepanning, and hydrogen-oxygen flame fusion performed in controlled, cleanroom environments to prevent devitrification (cristobalite phase transformation).
2. Comparative Material Science Matrix: Fused Quartz vs. Competing Substrates
Procurement directors and vacuum chamber designers must balance mechanical rigidity, optical transmission, thermodynamic tolerance, and gas outgassing rates. The following matrix contrasts clear fused quartz against alternative engineering glasses and technical ceramics commonly evaluated for gas manifold blocks.
| Physical / Thermal Parameter | Semiconductor Fused Quartz | Synthetic Fused Silica (JGS1) | Borosilicate 3.3 Glass | High-Purity Alumina (99.5% Al₂O₃) |
|---|---|---|---|---|
| Chemical Purity (SiO₂ / Primary Oxide) | ≥ 99.99% | ≥ 99.9999% | ~ 81% SiO₂ (13% B₂O₃) | ≥ 99.5% Al₂O₃ |
| Max Continuous Operating Temp (°C) | 1,100 °C | 1,150 °C | 450 °C | 1,600 °C |
| Max Short-Term Thermal Spike (°C) | 1,300 °C | 1,350 °C | 500 °C | 1,750 °C |
| Thermal Expansion Coeff. (20-320°C) | 5.5 × 10⁻⁷ /K | 5.2 × 10⁻⁷ /K | 32.5 × 10⁻⁷ /K | 80.0 × 10⁻⁷ /K |
| Thermal Shock Tolerance (ΔT) | > 1,000 °C (Quench safe) | > 1,050 °C (Quench safe) | 150 °C | 200 °C |
| Hydroxyl (OH⁻) Content Options | < 5 ppm to 30 ppm | < 1 ppm (Water-free) or ~1200 ppm | N/A (Complex compound) | N/A (Opaque ceramic) |
| Visual / Spectral Transparency | Deep UV to Near IR (260-2500nm) | Deep UV Excimer (185-2100nm) | Visible Spectrum (350-2000nm) | Completely Opaque (White/Ivory) |
| Machining Internal Micro-Channel Finish | Fire-polished Ra < 0.1 μm | Optical Fire-polish Ra < 0.05 μm | Mechanical polish Ra ≈ 0.4 μm | Lapped Ra ≈ 0.8 μm |
Future Procurement Trends for OEM Quartz Manifolds (2025–2030)
Global semiconductor supply chain shifts, localized wafer fabrication hubs, and rigorous environmental compliance are transforming quartz procurement models worldwide.
1. Transition to Monolithic Manifold Blocks
Traditional multi-joint welded manifolds rely heavily on manual flame-welding, which introduces subtle heat-affected zones (HAZ) and potential stress risers. Semiconductor OEMs are aggressively pivoting toward monolithically drilled quartz blocks. By utilizing 5-axis CNC diamond core grinding and ultra-short pulse femtosecond lasers, manufacturers carve continuous 3D internal fluid galleries directly inside a solid high-purity quartz billet, eliminating 80% of welded interfaces.
2. Total Cost of Ownership (TCO) & Extended Mean Time Between Clean (MTBC)
Procurement teams are shifting analysis from initial component purchase price to lifetime operational cost. Fused quartz manifolds engineered with controlled hydroxyl (OH) levels and flame-passivated inner bores resist micro-crack development caused by repeated in-situ NF3 and SF6 plasma cleaning cycles. This resistance extends replacement intervals from 6 months to over 24 months in continuous ALD lines.
3. Direct-from-Cluster OEM Supplier Integration
Due to wafer fab expansions across North America, Southeast Asia, and Europe, tier-1 equipment integrators bypass domestic intermediaries and establish direct supply partnerships with localized manufacturing hubs in Donghai, China. Direct factory engagement slashes tooling lead times from 16 weeks to under 15 days while maintaining exact 1-piece prototyping agility.
4. Helium Mass-Spectrometer Certification Mandates
Zero-tolerance policies for toxic precursor gas leaks (such as silane, phosphine, or metal-organic liquids) mean vacuum manifolds now require 100% helium mass-spectrometer leak certifications (< 1 × 10⁻⁹ mbar·l/s) prior to factory dispatch. Purchasing agreements increasingly mandate individual serialized test certificates and cleanroom vacuum packaging as standard deliverables.
5. Digital Twin CAD & Pre-Weld Thermal Modeling
To eliminate costly trial-and-error cycles in multi-port manifold assemblies, buyers provide parametric STEP models that undergo thermal stress simulation prior to torch work. Engineers calculate cooling shrinkage rates to maintain port-to-port pitch tolerances within ±0.1mm across 12-port headers, guaranteeing plug-and-play alignment inside cleanroom vacuum process chambers.
6. Closed-Loop Quartz Ingot Traceability
Environmental, Social, and Governance (ESG) guidelines in the tech sector demand transparent raw material chain-of-custody. Leading quartz manufacturers now verify the origins of natural pegmatite silica crystals, providing Inductively Coupled Plasma Mass Spectrometry (ICP-MS) purity assays verifying heavy metal and alkali impurity profiles below 15 ppm total.
Technological Evolution in Custom Quartz Glass Fabrication
From artisanal bench glassblowing to computer-controlled multi-axis laser processing: discover how modern engineering guarantees repeatable precision for complex manifold geometry.
State-of-the-Art Processing Methodologies
Historically, constructing a multi-branch quartz manifold was an empirical craft. Skilled glassblowers used handheld hydrogen-oxygen torches to attach branch tubes onto a primary header pipe. While functional for standard chemistry lab condensers, this approach created variable wall thickness at intersections, micro-scalloping, internal flame haze (silica soot), and high localized residual stresses that often fractured during rapid thermal cycling.
Today, advanced OEM quartz fabrication combines automated robotic glass lathes with multi-stage computerized thermal processing:
- Laser Trepanning & Micro-Drilling: High-energy CO2 and ultraviolet picosecond lasers cut port orifices with micrometer accuracy, creating clean pilot holes without edge micro-chipping or subsurface micro-fissures.
- Hydrogen-Oxygen Precision Lathe Fusion: Headers and ports rotate synchronously on multi-chuck quartz glass lathes. Computerized flame jets maintain exact fusing temperatures (1,700°C to 1,900°C), creating uniform fillet radii at tube intersections that optimize laminar gas flow and prevent flow stagnation.
- Automated Full-Immersion Annealing: Completed manifolds undergo multi-hour computer-controlled annealing cycles in refractory ovens at 1,150°C to 1,215°C. This eliminates internal mechanical stresses induced during welding. Stress profiles are inspected using cross-polarized optical polariscopes, guaranteeing residual birefringence below 5 nm/cm.
- Internal Chemical Etching & Fire Polishing: Specialized hydrofluoric/nitric acid pickling baths dissolve surface micro-defects, followed by controlled flame polishing to achieve an ultra-smooth internal finish (surface roughness Ra ≤ 0.1 μm) that minimizes chemical condensation and bacterial adhesion.
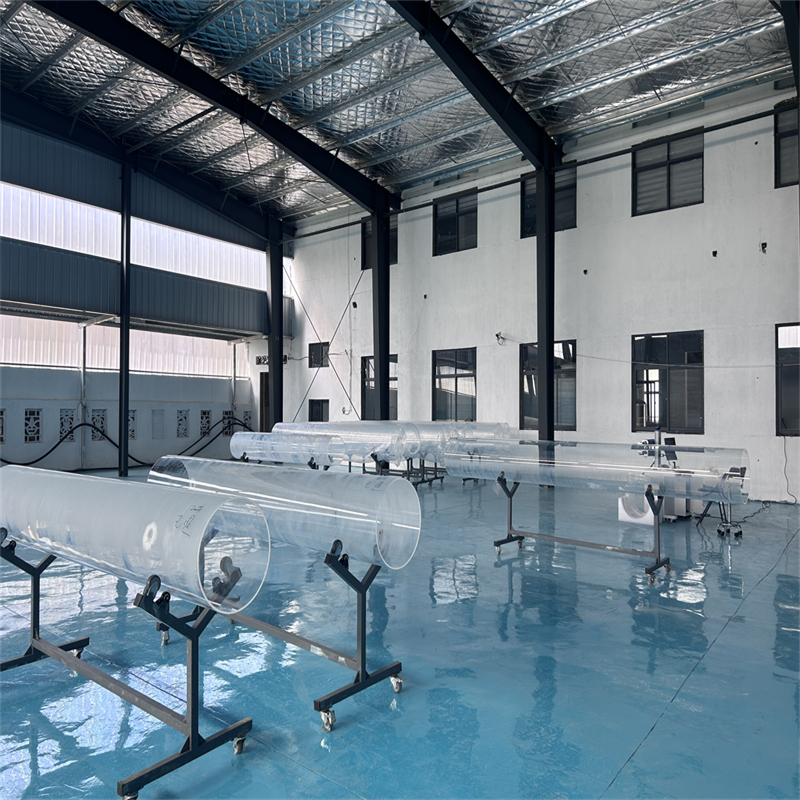
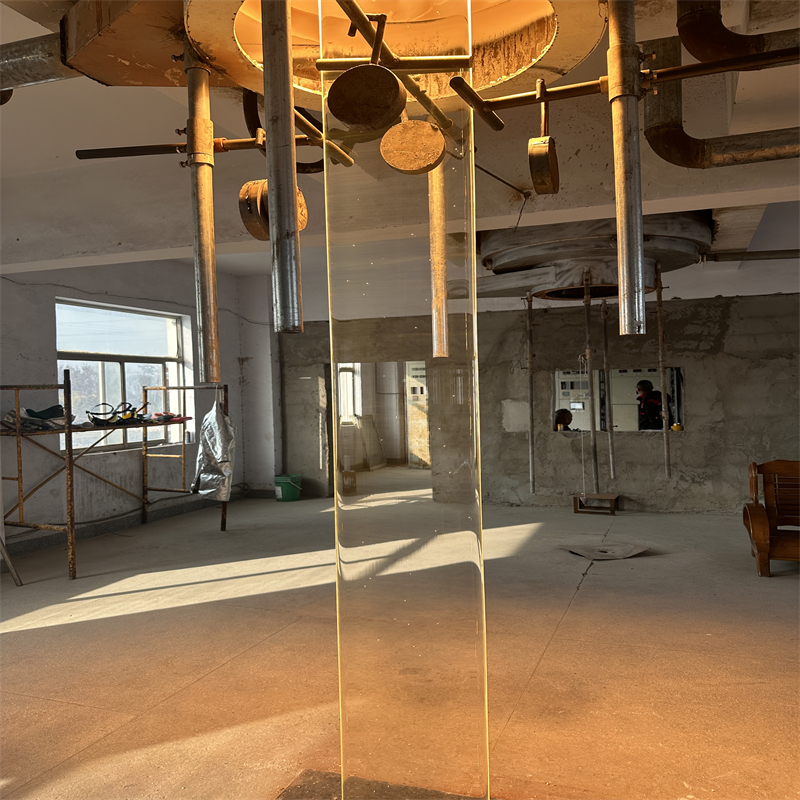
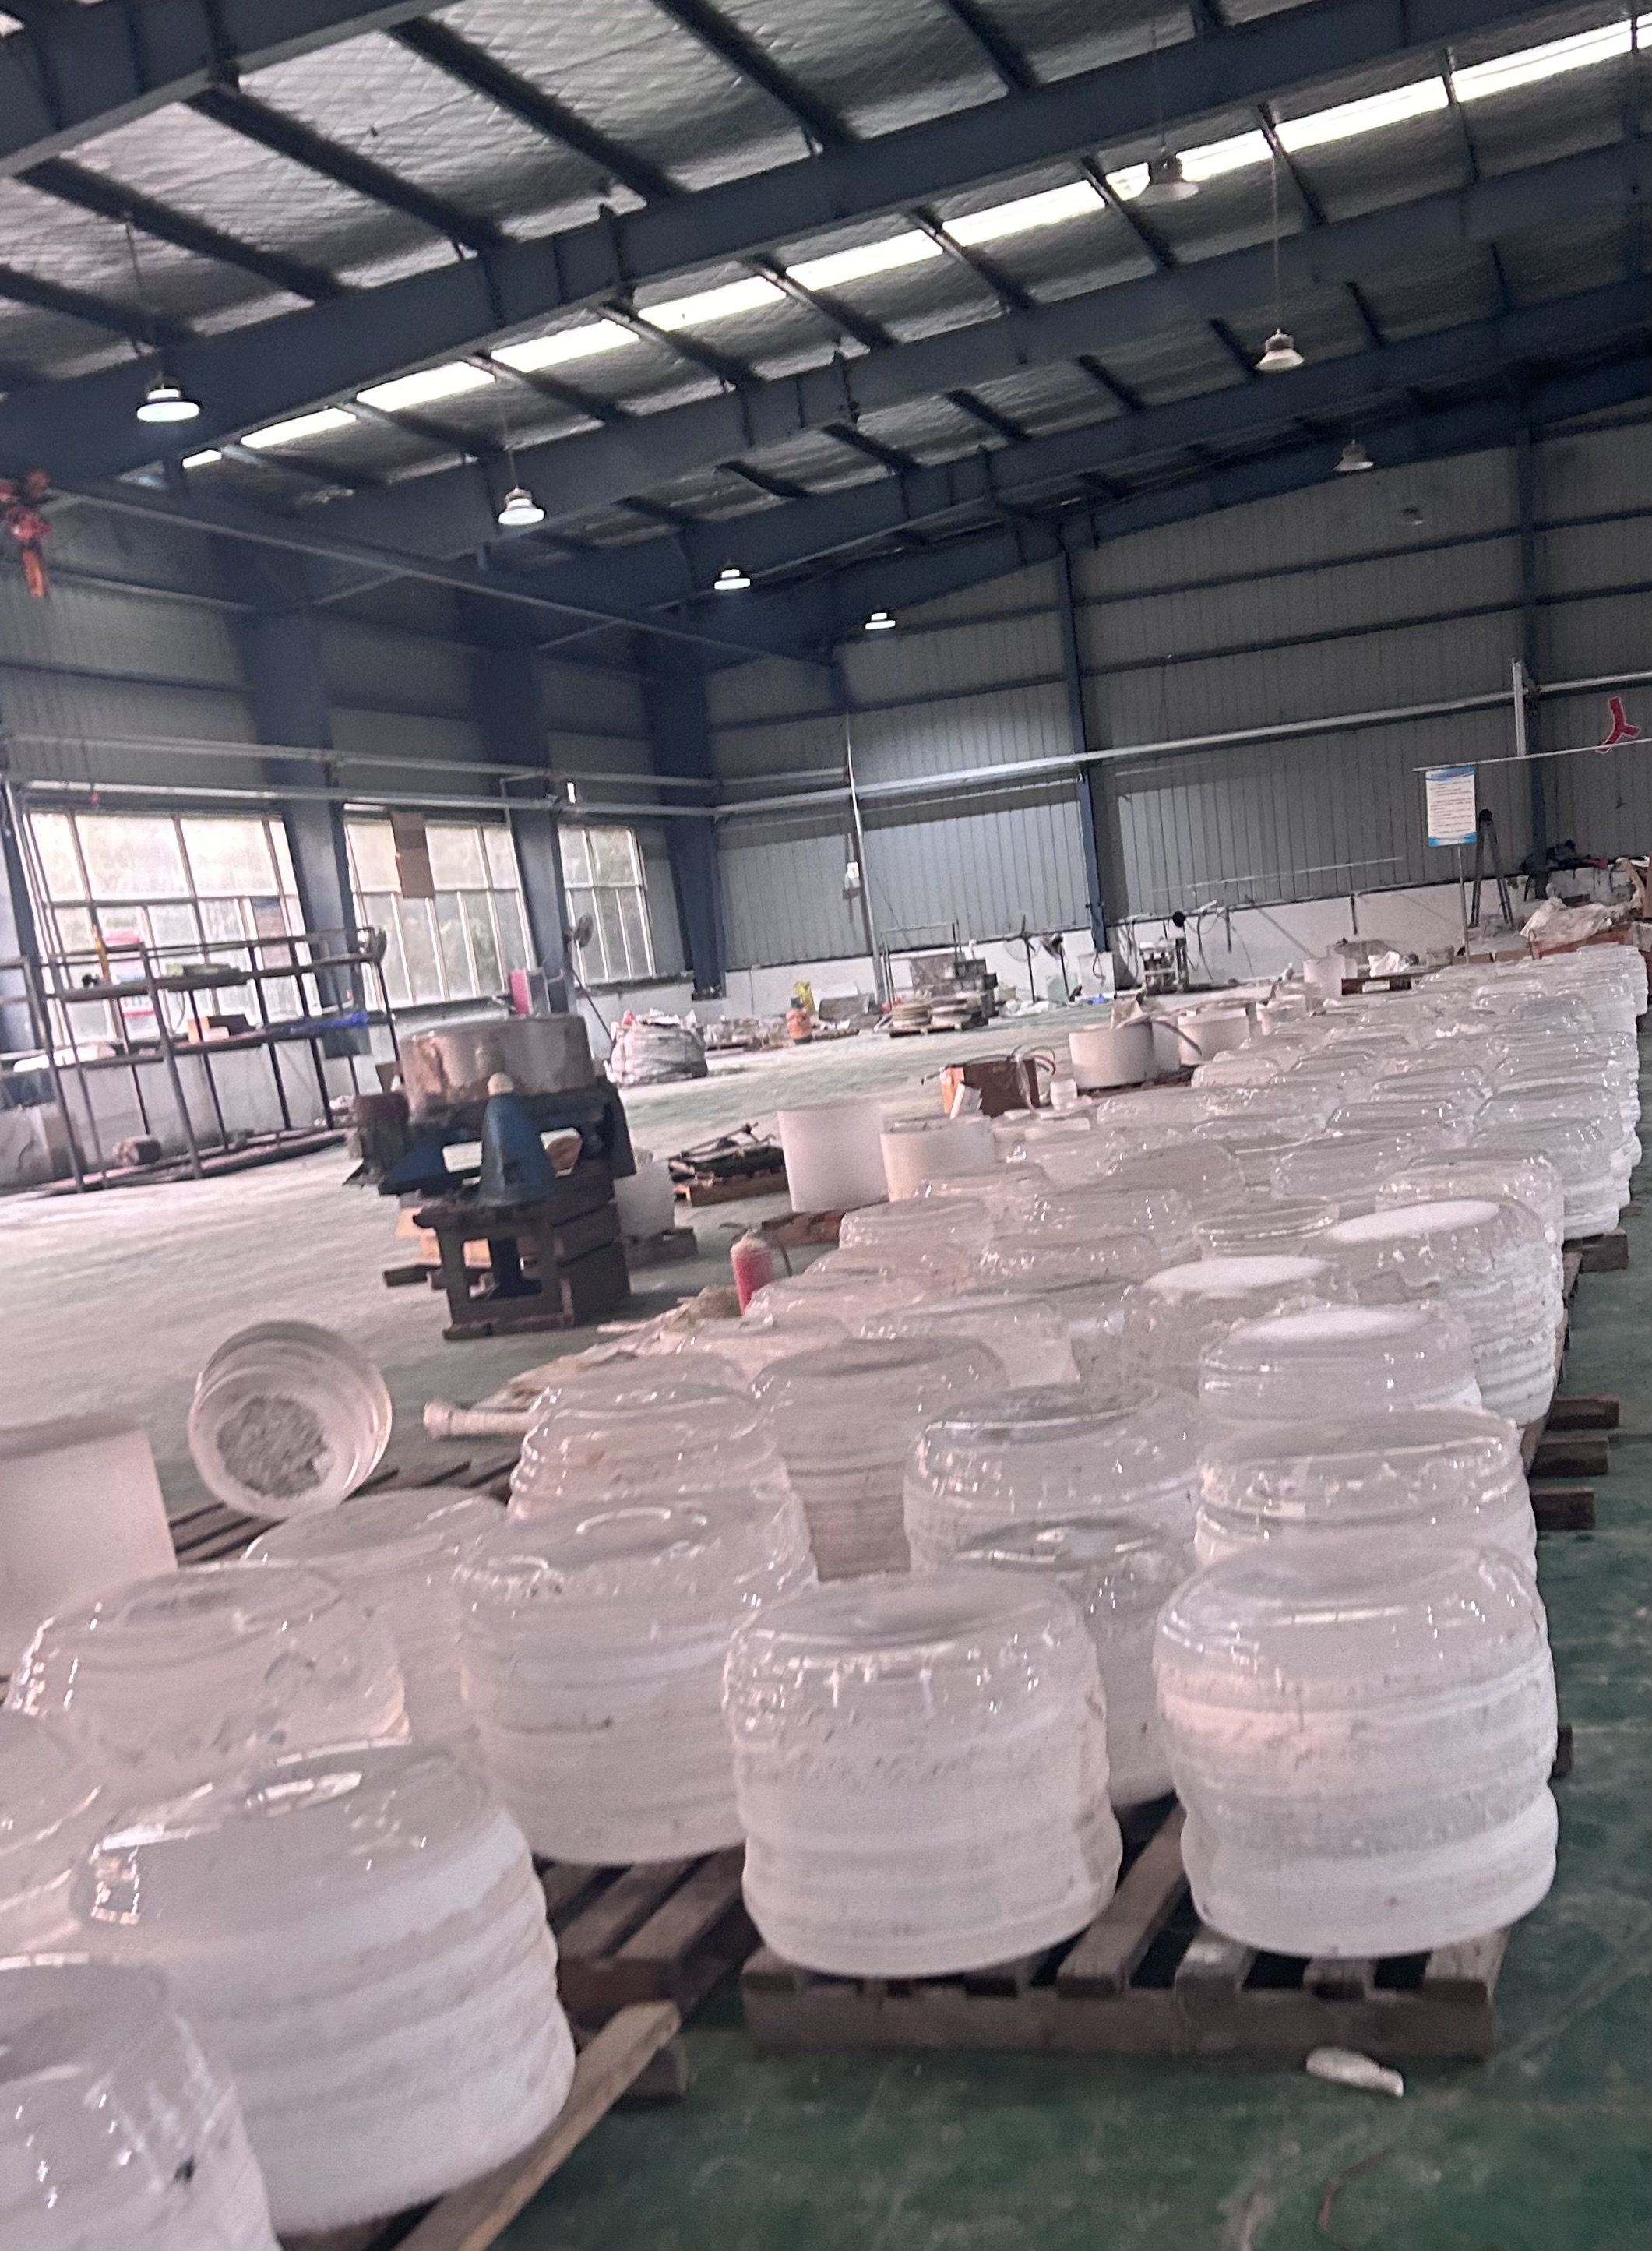
Factory Shop Floor & Production Verification
Authentic workshop operations from Lianyungang Zelvo Quartz Products Co., Ltd. in Donghai, Jiangsu.
Why Global Engineering Teams Partner with Zelvo Quartz
Headquartered in Donghai County, China's quartz capital, Lianyungang Zelvo Quartz Products Co., Ltd. blends geographic material cost advantages with top-tier CNC machining.
Located at the origin of China's highest grade silica deposits in Donghai, Jiangsu. We control raw ingot sourcing directly, eliminating secondary markups and guaranteeing raw stock reserves for quick turnaround times.
Our sales engineering team does not use call-center scripts. You interact directly with quartz fabrication veterans boasting 10+ years of bench experience. We review 2D PDF or 3D STEP drawings and provide actionable feedback promptly.
We welcome R&D experimental trials, university research prototypes, and replacement lines for obsolete semiconductor tools starting from a single unit, scaling smoothly to production volumes of thousands.
From core ingot sawing, diamond grinding, laser micro-drilling, and slotting to specialized oxy-hydrogen welding, flange fusing, polariscope stress-relief, and cleanroom vacuum packaging.
Have an Engineering Drawing or Custom Manifold Specification?
Send your dimensional tolerances, working gas temperatures, and connection flange types. Our technical department will analyze your blueprint and return a detailed DFM (Design for Manufacturability) feasibility report and pricing quotation.
Custom Quartz Glass Manifold Procurement FAQs
Answers to key technical questions encountered by procurement managers, process engineers, and vacuum chamber designers.
What raw quartz grades do you utilize for custom manifold assemblies?
What dimensional and angular tolerances can your workshop maintain on complex manifolds?
How do you verify and eliminate residual stress after flame-welding quartz manifold branches?
What vacuum flange connections and port terminations can be integrated?
How do you ensure zero contamination and leak tightness before overseas shipment?
Can you assist in reverse-engineering an obsolete quartz manifold without original CAD files?
What trade terms and payment methods are supported for international deliveries?
Start Your Custom Quartz Glass Manifold Fabrication Today
Direct factory pricing. Certified 99.99% purity. Comprehensive feasibility reviews within 2 hours. Partner with an experienced manufacturer based in Donghai, Jiangsu.