Precision Fused Quartz Components for Critical Thermal Assemblies
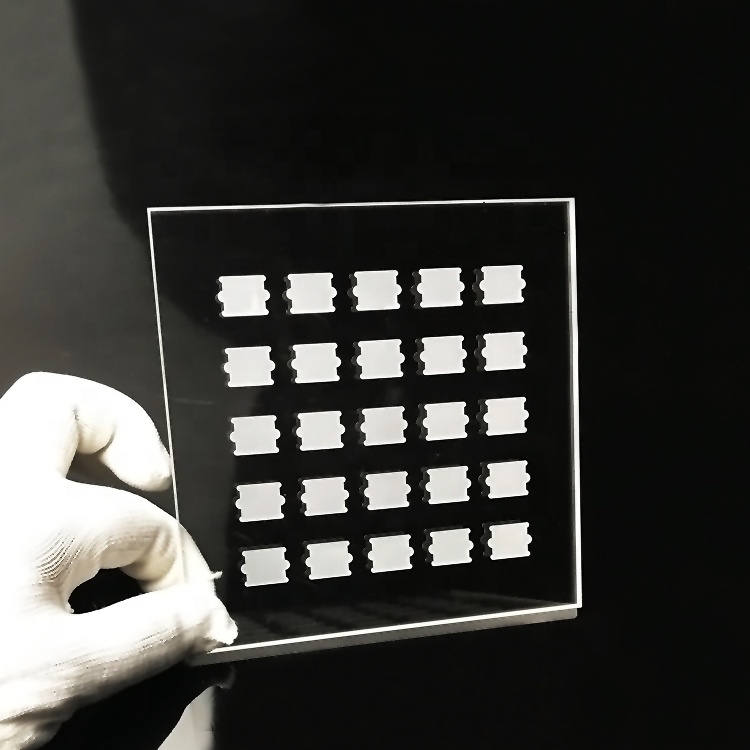
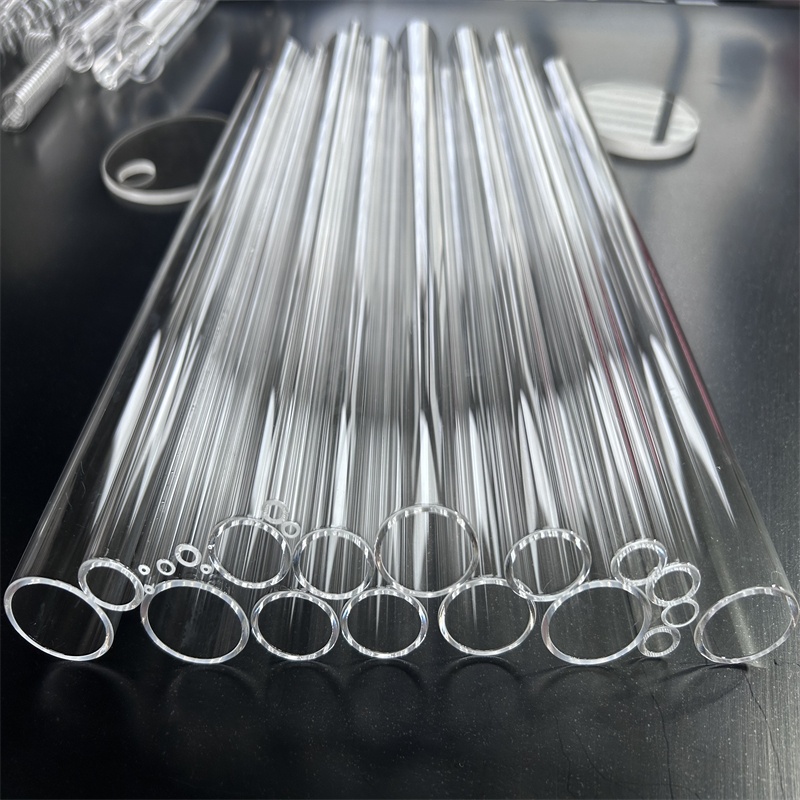
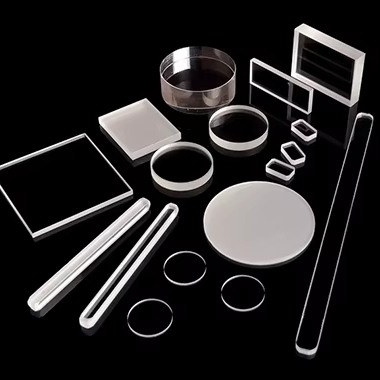
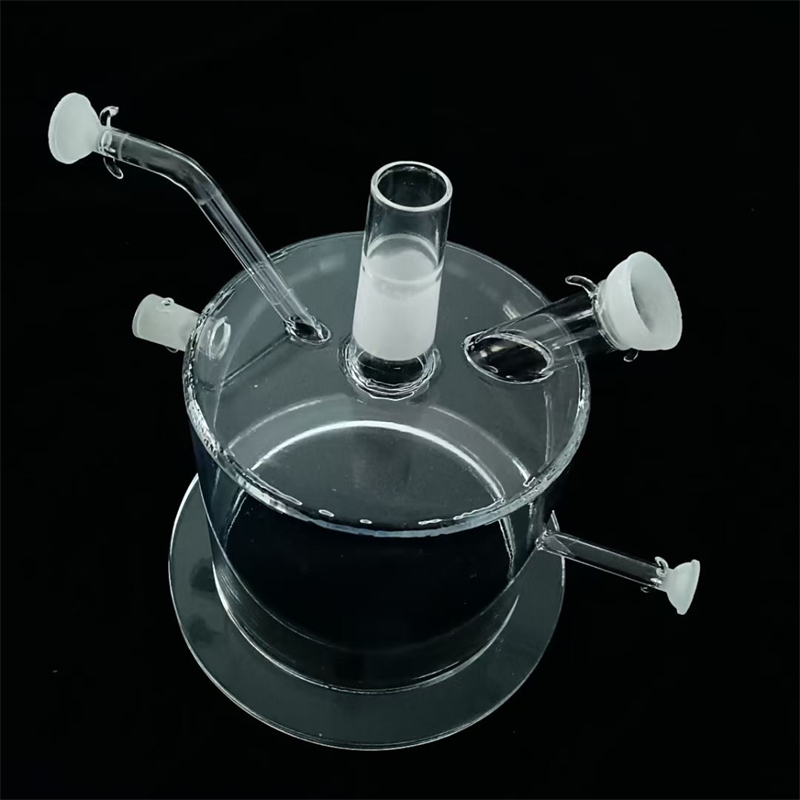
Manufactured from optical and opaque quartz with ≥99.99% SiO₂ purity. Every unit undergoes strict laser dimensional verification and ultrasonic cleaning before international dispatch.
Thermodynamics & Material Mechanics of Opaque (Milky) Quartz
A rigorous examination of micro-bubble scattering, infrared attenuation, and thermal shock survivability in industrial furnace architectures.
1. Microstructure and Mie Scattering Phenomena in Opaque Fused Silica
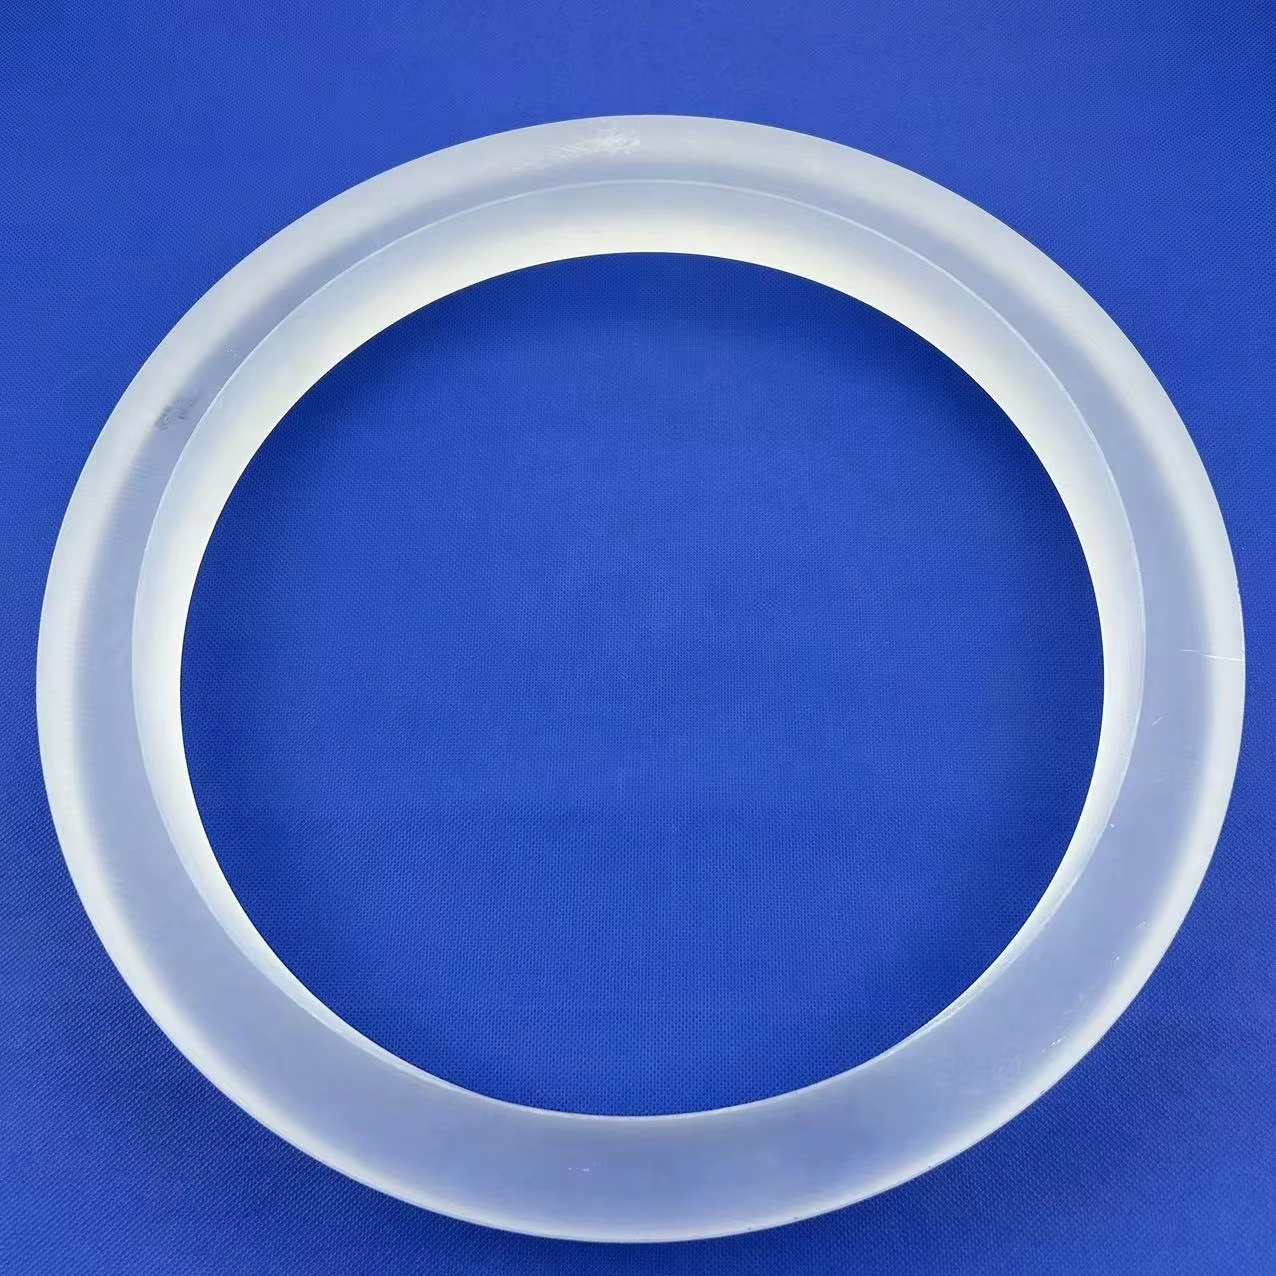
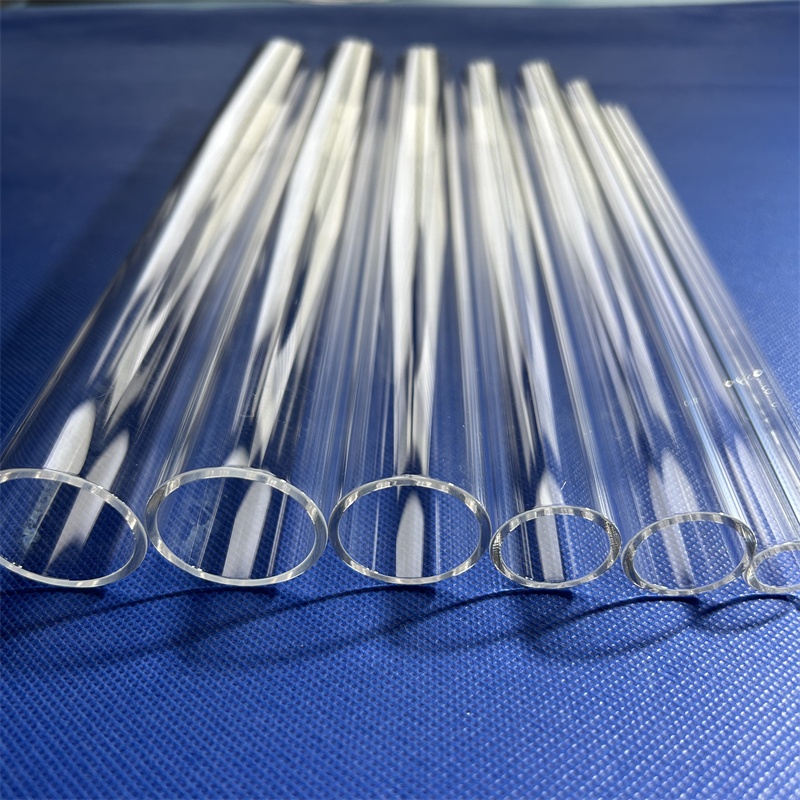
Milky quartz tubes (often termed opaque fused silica or translucent quartz glass) are engineered through continuous thermal fusion of ultra-pure natural quartz sand. Unlike transparent fused silica, milky quartz incorporates a controlled volumetric distribution of microscopic closed gaseous pores (diameters typically ranging from 5 to 50 micrometers). These inclusions do not represent impurities; rather, they serve as powerful refractive scattering boundaries governed by Mie scattering principles.
When high-intensity infrared radiation (wavelengths λ between 1.0 µm and 4.5 µm) encounters the tube wall, the refractive index mismatch between the gaseous voids (n ≈ 1.0) and the surrounding amorphous SiO₂ matrix (n ≈ 1.46) causes extensive multi-directional diffuse scattering. This prevents direct radiant thermal pass-through, converting intense localized heat into uniform omnidirectional radiant emission. Consequently, milky quartz acts as an exceptional infrared radiant equalizer and thermal barrier, shielding external assemblies while maintaining outstanding isothermal stability inside thermal chambers.
2. Thermal Shock Resistance and Devitrification Kinetics
The operational longevity of furnace tubes in rapid-cycling thermal regimes is fundamentally limited by thermal stress cracking. Milky quartz retains an extraordinarily low coefficient of thermal expansion (CTE) of approximately 5.5 × 10⁻⁷ K⁻¹ between 20°C and 1000°C. This allows components to survive severe water quench tests from 1100°C without catastrophic macro-cracking.
Furthermore, high-purity milky quartz manufactured under vacuum-thermal fusion exhibits low hydroxyl (OH⁻) content, which substantially suppresses the kinetics of cristobalite phase transformation (devitrification) above 1150°C. In heavy industrial environments where trace alkali elements (Na, K, Ca) act as crystallization catalysts, our precision-purified SiO₂ glass provides an extended service life by maintaining structural amorphous integrity under extreme thermal gradients.
| Physical / Thermal Parameter | Milky Quartz (Opaque Fused Silica) | Clear Fused Quartz (Type II/III) | Recrystallized Alumina (99.7% Al₂O₃) | Borosilicate Glass 3.3 |
|---|---|---|---|---|
| Density (g/cm³) | 2.05 – 2.18 | 2.20 | 3.90 | 2.23 |
| Coefficient of Thermal Expansion (10⁻⁷/K) | 5.4 – 5.6 | 5.5 | 80.0 | 33.0 |
| Max Continuous Temperature (°C) | 1100 – 1150 | 1150 | 1650 | 450 |
| Short-Term Thermal Peak (°C) | 1300 | 1300 | 1800 | 500 |
| Infrared Transmission Profile | High Diffuse Scattering (Thermal Shield) | Direct Transmission (>90% NIR) | Opaque / High Thermal Mass | Cut-off at 2.7 µm |
| Thermal Shock Resistance | Exceptional (Water Quench >1100°C) | Exceptional | Moderate / Risk of Fracture | Poor (ΔT ≈ 100°C) |
| Acid Resistance (except HF & Hot H₃PO₄) | Class 1 / Inert | Class 1 / Inert | High | Class 1 |
3. Mechanical Machining and Custom Geometrical Tolerances
Processing opaque quartz requires advanced diamond-tooled CNC machinery due to its Mohs hardness of 5.5–6.5 and internal pore structure. Zelvo Quartz employs computerized slicing, precision water-cooled core drilling, circumferential grooving, and high-temperature hydrogen-oxygen flame welding. Our manufacturing tolerance standards comply with ISO 2768-m, achieving tube wall thickness concentricity within ±0.15 mm and length tolerances within ±0.5 mm for custom flanged installations.
Industrial Application Scenarios Across the Narva & Ida-Viru Corridor
From the Auvere power generation complex to synthetic fuel pilot facilities and metal fabrication plants, our milky quartz components meet the rigorous demands of northeastern Estonia.
Thermal Power Generation & Flue Gas Monitoring
In the high-capacity thermal boilers operated around Narva, high-temperature gas monitoring demands protective sheaths capable of withstanding corrosive sulfurous gases (SO₂/SO₃) and abrasive ash particulates. Our thick-wall opaque quartz tubes protect thermocouple assemblies and optical pyrometers against localized erosion, thermal shock, and chemical slagging up to 1150°C.
Oil Shale Retorting & Synthetic Pyrolysis Reactors
Ida-Viru's proprietary solid heat carrier (Enefit technology) and synthetic chemical conversion plants utilize advanced continuous pyrolysis chambers. Milky quartz serves as custom muffle tubes, reactant delivery pipes, and electric heating core shields where diffuse infrared heating prevents localized hot spots that lead to undesired hydrocarbon coking.
Industrial Heating Elements & Vacuum Furnaces
Regional machinery builders and metallurgical workshops in Narva and Kohtla-Järve require twin-bore and flanged milky quartz tubes as heavy-duty infrared heating sleeves. The diffuse scattering profile shields nichrome and Kanthal elements from physical contamination while maximizing radiative energy efficiency across heating chambers.
Clean-Tech & Green Hydrogen Pilot Facilities
As part of Estonia's Just Transition economic transformation, new pilot manufacturing hubs in Ida-Viru are deploying high-temperature solid oxide electrolyzers (SOEC) and synthesis reactors. Milky quartz tubes provide non-conductive, chemically inert thermal barriers capable of operating in pressurized hydrogen and steam mixtures without embrittlement.
Industrial Water Purification & Ozone Diffusion
Narva’s industrial chemical plants and municipal district facilities utilize ozone gas injection systems for water purification. Porous and perforated quartz contactor tubes supply aggressive oxidizers without risk of surface leaching, structural breakdown, or heavy-metal contamination, outlasting high-grade stainless steels by multiple factors.
Analytical Laboratories & Research Test Cells
Laboratories testing oil shale derivatives, catalytic conversions, and battery precursors throughout Narva, Tartu, and Tallinn rely on our BET sample tubes, XRD quartz plates, and combustion reactor tubes for reproducible, contamination-free thermal testing under aggressive chemical vapor deposition conditions.
Procurement Evolution in Ida-Viru: Resilience & Green Transition
Understanding shifting technical specifications, EU standards, and global factory-direct logistics for Estonia's evolving industrial sector.
The Just Transition Fund (Õiglase Ülemineku Fond) Impact on Equipment Specifications
Estonia’s Ida-Viru County is currently navigating one of Europe’s most ambitious regional industrial transformations. Backed by the European Union’s Just Transition Fund (ÕUF) with over €350 million in dedicated funding, the region is modernizing legacy thermal assets while aggressively investing in advanced battery chemical processing, circular economy manufacturing, and synthetic fuels. This transformation demands a rapid overhaul of high-temperature processing equipment.
Procurement engineers in Narva are transitioning from legacy standard-tolerance ceramic materials to customized, high-purity fused silica and quartz components. Modern chemical syntheses require zero trace metal leaching (specifically keeping Fe < 1 ppm, Al < 15 ppm, and Na < 1 ppm) to prevent catalyst poisoning during high-temperature reactions. As local enterprises upgrade existing boiler lines and construct new clean-tech pilot facilities, the demand for precision OEM/ODM milky quartz tubes with customized flange couplings, laser-drilled gas distribution ports, and specific infrared scattering profiles has increased significantly.
Navigating Direct Factory Sourcing vs. Intermediary Supply Chains
Historically, Estonian industrial facilities sourced fused quartz components through multi-tiered European distributors, resulting in extended lead times of 12 to 18 weeks and inflated procurement costs. By partnering directly with integrated OEM/ODM manufacturers based in Donghai—China’s primary crystal capital and quartz processing hub—Narva engineering teams achieve substantial operational advantages:
1. Direct Engineering Communication: Technical drawings are evaluated directly by quartz glassblowers and CNC machinists, eliminating misunderstandings regarding critical dimensional tolerances, chamfering, and annealing schedules.
2. Rapid Prototyping (MOQ 1 Piece): Rather than committing to large batch runs, research teams and maintenance managers can order single-piece prototypes for custom retrofit validation.
3. Certified Quality & Compliance: Direct delivery with comprehensive factory inspection documentation, material spectroscopic test reports, and compliance certificates for RoHS 3 (Directive 2015/863/EU) and REACH (Regulation EC 1907/2006).
Why Leading Industrial Buyers Trust Zelvo Quartz
Decades of specialized fused silica engineering, state-of-the-art precision equipment, and dedicated export logistics tailored for European industrial standards.
Certified 99.99% SiO₂ Purity
Raw materials sourced from Donghai’s high-purity natural silica deposits. Refined through proprietary thermal chemical processes ensuring trace metallic elements remain below critical PPM thresholds.
Full Drawing-Based Fabrication
Complete secondary machining capabilities including 5-axis laser cutting, micro-hole drilling, ultrasonic polishing, slotting, precision lathe threading, and automated flame bending.
Rapid Engineering Turnaround
Our sales engineering team provides full drawing reviews and feasibility feedback within 2 hours. Rapid prototype shipping ensures replacement parts reach European facilities without production halts.
Zero-Breakage Export Packaging
Engineered multi-tier packaging utilizing custom-molded high-density PE foam, vacuum-sealed barrier films, and reinforced plywood crates compliant with ISPM-15 international transit regulations.
Engineering & Procurement FAQ for Narva Industrial Clients
Clear, definitive answers to technical, logistical, and compliance questions regarding milky quartz sourcing for Estonian operations.
What is the key functional difference between milky (opaque) quartz tubes and clear quartz tubes in furnace applications?
What is the maximum operating temperature of milky quartz tubes, and how can we prevent devitrification?
Can Zelvo Quartz fabricate milky quartz tubes according to custom CAD/PDF engineering drawings?
What is the Minimum Order Quantity (MOQ) for prototypes and pilot plants in Ida-Viru County?
How do you ship fragile quartz products to Narva, Estonia, and what Incoterms are supported?
Are your quartz components compliant with European Union regulations (RoHS, REACH)?
Need Custom Milky Quartz Tubes for Your Narva Installation?
Submit your technical drawings or dimensional requirements. Our senior quartz engineering team will review your specifications, verify thermal tolerances, and return a competitive factory-direct proposal within 2 hours.